القص بالليزر مقابل القص بالبلازما: مقارنة شاملة
29 يونيو 2026
Laser Cutting vs Plasma Cutting: A Complete Comparison
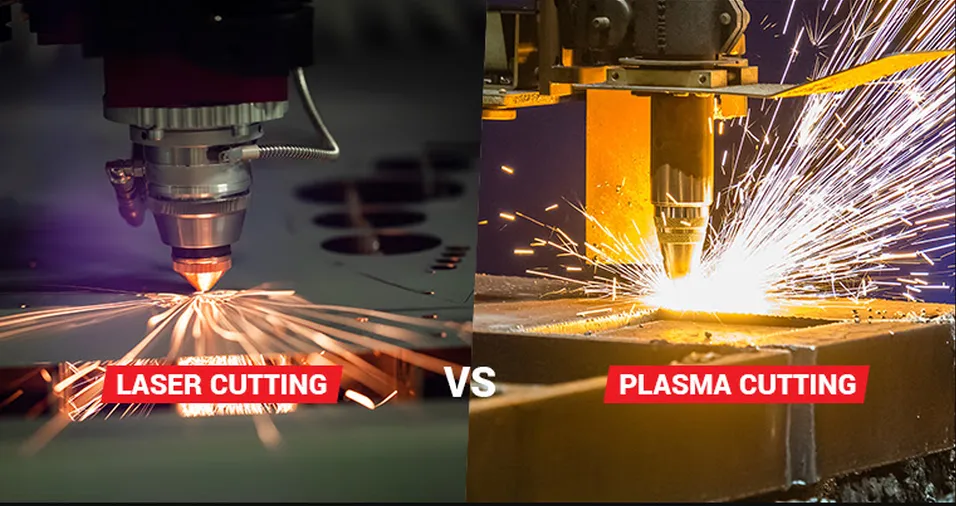
Speed, Precision, Cost, Applications & Which Technology is Right for Your Shop
Laser vs Plasma: Complete Technology Comparison
You need to cut metal. Fast. Precisely. Without breaking the bank. But there are two technologies competing for your attention: laser cutting and plasma cutting.
Which one wins? The answer isn't simple-because it depends on what you're cutting, how much you're cutting, and what quality you need.
This guide compares laser and plasma cutting across every dimension: speed, precision, cost, materials, applications, and real-world performance. By the end, you'll know exactly which technology is right for your fabrication shop.
1. Technology Overview: How Each System Works
Fiber Laser Cutting Technology
A fiber laser generates coherent light at 1064 nanometers wavelength using rare-earth doped fiber as the gain medium. The system:
- Produces high-power laser light (typically 1.5-6kW for industrial applications)
- Focuses through a lens into a spot as small as 0.1mm diameter
- Directs the beam via fiber optic cable to the cutting head
- Creates localized heating to vaporization temperature (1,500-2,000°C for most metals)
- Assist gas (nitrogen or oxygen) blows away vaporized material
- Results in a clean cut with minimal heat-affected zone (HAZ)
Key Advantage: The beam is tiny (0.1mm vs plasma's 5-10mm), so the heat is extremely localized. This is why laser is so precise (±0.05mm) and produces almost zero dross.
Plasma Cutting Technology
Plasma cutting ionizes a pressurized gas (argon, nitrogen, or oxygen) with electrical current to create a high-temperature arc. The process:
- Initiates an arc between torch electrode and material (15,000-20,000°C)
- High-temperature plasma jet accelerates at 6,000+ m/s toward the material
- Arc melts a large area with kerf width of 1.5-2.5mm
- High-velocity gas jet momentum blows molten metal away from the cut
- Bottom edge often has re-solidified metal re-attaching (dross formation)
- Requires secondary deburring (15-30 minutes per batch)
Key Advantage: The arc is powerful enough to cut through thick, conductive materials quickly. Less focused energy means less precision but faster on heavy work 30m
2. Performance Comparison: Speed by Material & Thickness
Speed is where the technologies diverge most dramatically. The crossover point is around 12-15mm-below that, laser dominates; above that, plasma becomes competitive and then wins outright.
Speed Data: Mild Steel Cutting
| Material Thickness | Laser Speed (m/min) | Plasma Speed (m/min) | Winner & Ratio |
|---|---|---|---|
| 1mm | 6-8 | 1-1.5 | Laser 5-8x faster |
| 3mm | 4-6 | 1.5-2 | Laser 2-4x faster |
| 6mm | 2.5-3.5 | 2-2.5 | Laser 1.2-1.5x faster |
| 12mm | 1.5-2 | 2-3 | Plasma 1.2-1.5x faster |
| 20mm | 0.8-1.2 | 3-4 | Plasma 3-6x faster |
| 30mm+ | Impractical | 4-6 | Plasma only viable |
Stainless Steel & Specialty Materials
| Material | Laser Capability | Plasma Capability | Best Choice |
|---|---|---|---|
| Stainless Steel | Excellent (2-3x faster, clean edges) | Good (rough edges, needs deburring) | Laser |
| Aluminum | EXCELLENT (reflective metal) | ✗ Cannot cut | Laser only |
| Copper/Brass | EXCELLENT (highly reflective) | ✗ Cannot cut | Laser only |
| Galvanized Steel | Good | Good (higher gas cost) | Either (thickness dependent) |
3. Cutting Quality & Edge Finish Analysis
Precision Metrics
| Quality Metric | Fiber Laser | Plasma |
|---|---|---|
| Positional Tolerance | ±0.05-0.1mm | ±1-2mm |
| Kerf Width | 0.1-0.15mm | 1.5-2.5mm |
| Heat Affected Zone | 0.1-0.5mm | 5-10mm |
| Edge Dross/Burr | Virtually none | Always present |
| Edge Finish (Ra) | 0.4-0.8μm (mirror smooth) | 3.2-6.3μm (requires finishing) |
What This Means for Your Shop
Laser Advantage: Parts are ready to use immediately. No deburring, no secondary machining, no rework. If tolerances matter (±0.1mm), laser is the only choice. Eliminates 15-30 minutes of deburring labor per batch.
Plasma Consideration: Parts need 15-30 minutes of deburring per batch. For loose-tolerance work (brackets, guards, filler plates), this is acceptable. For tight tolerance assemblies, it's not viable.
4. Material Compatibility: What Each Can & Cannot Cut
| Material | Laser | Plasma | Best Choice |
|---|---|---|---|
| Mild/Carbon Steel | ✓ Excellent | ✓ Excellent | Laser <12mm, Plasma >20mm |
| Stainless Steel | ✓ Excellent (2-3x faster) | ✓ Good (rough edges) | Laser preferred |
| Aluminum | ✓ EXCELLENT | ✗ Cannot cut | Laser only |
| Copper/Brass | ✓ EXCELLENT | ✗ Cannot cut | Laser only |
| Galvanized Steel | ✓ Good | ✓ Good (higher gas cost) | Either, based on thickness |
| Cast Iron | ⚠ Difficult | ✓ Good | Plasma |
5. Industry Applications
Industries That Choose Laser
HVAC & Sheet Metal (Ductwork)
Laser dominates because most work is 1-4mm aluminum ductwork. Speed advantage = 3-5x faster production. Material never needs deburring. Cost-per-part is lowest with laser.
Automotive Suppliers
Tight tolerances (±0.1mm) are standard. Laser achieves these naturally. No secondary operations needed. Parts go straight to assembly line.
Job Shops with Variety
Mixed materials (aluminum, stainless, mild steel). Laser cuts all reflective metals-plasma cannot. Ability to handle copper/brass components is critical.
Architectural Metalwork
Complex geometries, decorative cuts, tight corners. Laser delivers 0.1mm kerf allowing intricate designs. Plasma's 2mm kerf is too wide for fine detail.
Electronics & Enclosures
Stainless steel panels, aluminum housings. Need mirror-smooth edges, no secondary finishing. Laser delivers out-of-the-box quality.
Industries That Choose Plasma
Heavy Structural Fabrication
Steel beams, columns, plates 30-50mm thick. Plasma is only practical choice-laser would require 10kW+ power and still be slow. Initial cost is primary constraint, not consumables.
Ship Building & Maritime
Cutting thick hull plates, frames, stiffeners. Precision isn't critical-plasma speed on heavy steel is unmatched.
Large Frame Construction
Steel structures where edge quality isn't critical. Work can tolerate 1-2mm tolerances. Lower upfront cost justifies plasma choice.
Pipe & Tube Cutting
Cutting structural tubes, pipes 5-20mm wall thickness. Plasma speed acceptable for this application.
6. ROI & Payback Period Analysis
Expected Case: 5-Year Laser ROI
221%
5-Year Cumulative ROI$221K
Expected Net Profit (5 yrs)~14 months
Break-Even Point44% per year
Average ROI (5-year period)Key Assumptions (Expected Case)
- Machine Investment: $100K USD (AED 366K)
- Average Net Profit: $1,550/month
- Operating Hours: 8 hrs/day, 22 days/month
- Skilled Operator: 1 person
- Utilization: Moderate (not at max capacity)
Real-world scenarios vary:
- Best Case (high utilization): Break-even 9 months, ROI exceeds 400% in 5 years
- Expected Case (moderate utilization): Break-even 14 months, 221% ROI in 5 years
- Conservative Case (low utilization): Break-even 24 months, 100% ROI in 5 years
7. Advantages & Disadvantages
✓ Laser Advantages
- 3-5x faster on thin metals
- Superior precision (±0.05mm)
- Zero dross, no deburring
- Cuts reflective metals (aluminum, copper, brass)
- 60-75% lower consumable costs
- Minimal maintenance
- Better edge quality for next operations
- Lower total cost of ownership over 5 years
✗ Laser Disadvantages
- Higher initial investment ($100K-$250K)
- Slower on very thick materials (30mm+)
- Requires skilled operators
- More complex maintenance
- Setup costs higher
✓ Plasma Advantages
- 3x lower initial investment
- Faster on thick materials (30mm+)
- Handles extremely thick plates reliably
- Simpler technology, easier to learn
- Proven in heavy fabrication for decades
- Lower upfront capital requirement
- Works on cast iron & rough materials
✗ Plasma Disadvantages
- Cannot cut reflective metals reliably
- Lower precision (±1-2mm)
- Always produces dross (requires deburring)
- Large HAZ (5-10mm) affects material properties
- High consumable costs ($8K-$15K/year)
- Frequent maintenance (weekly consumable changes)
- Requires secondary finishing labor
- Higher total operating cost
Decision Matrix: How to Choose
Choose Laser If Your Shop: Choose Plasma If You
- Cuts primarily <12mm sheet metal (80% of work)
- Processes aluminum, copper, brass regularly
- Requires tight tolerances (±0.1mm or better)
- Wants to eliminate secondary deburring labor
- Values fast turnaround on diverse jobs
- Can commit to 18-24 month ROI timeline
- Values edge quality and material integrity
- Cuts primarily 30mm+ structural steel
- Needs lowest possible upfront capital
- Works on heavy fabrication/construction
- Tolerates loose tolerances (1-2mm acceptable)
- Can handle secondary deburring operations
- Focuses on speed over edge finish
- Has limited capital for equipment investment
FAQ: Your Top Questions Answered
Can laser cut thick metals like plasma?
Fiber lasers use focused light energy, which becomes increasingly difficult to deliver through thick material. The kerf width also grows with material thickness, reducing material utilization.
Laser Performance by Thickness
| Thickness | Performance | Notes |
|---|---|---|
| 0-6mm | Excellent | Fastest option available |
| 6-12mm | Very Good | Still 2-3x faster than plasma |
| 12-20mm | Acceptable | Starting to slow down |
| 20-30mm | Marginal | Very slow, economically questionable |
| 30mm+ | Not Recommended | Plasma 2-3x faster |
Which is safer to operate?
Both are safe when properly guarded. Laser requires better eye protection; plasma requires fume extraction. No clear winner
How much training do operators need?
Both are safe when properly guarded. Laser requires better eye protection; plasma requires fume extraction. No clear winner.
Safety Comparison
| Safety Aspect | Laser | Plasma |
|---|---|---|
| Eye Safety | Requires Class 4 enclosure | Lower risk |
| Fume/Smoke | Minimal | Significant |
| Electrical Hazard | Low voltage | High voltage (400V) |
| Heat Output | Localized | High ambient (35-50°C) |
| Noise Level | ~85 dB | ~95-105 dB |
Can I cut stainless steel on both?
Yes, both cut stainless steel easily. Laser is faster for thin (<6mm). Plasma is faster for thick (>20mm).
Stainless Steel Cutting Speed
| Thickness | Laser Speed | Plasma Speed | Winner |
|---|---|---|---|
| 1mm | 5-8 m/min | 1-2 m/min | Laser (3-5x) |
| 3mm | 3-5 m/min | 1-2 m/min | Laser (2-3x) |
| 6mm | 2-3 m/min | 1.5-2.5 m/min | Laser |
| 12mm | 1-1.5 m/min | 2-3 m/min | Plasma |
| 20mm+ | 0.5-0.8 m/min | 4-6 m/min | Plasma (4-5x) |
Edge Quality Differences
Laser on Stainless:
- Mirror-smooth edges
- Minimal HAZ
- No secondary finishing
- ±0.1mm tolerance
Plasma on Stainless:
- Slightly rougher
- Dross present
- Requires deburring
- ±1-2mm tolerance
How Much training do operators need?
Laser: 40-80 hours. Plasma: 30-60 hours. Both require ongoing certification in UAE/GCC.
Laser Operator Training (40-80 hours)
Initial Certification (40 hours):
- Basic laser physics & fiber laser technology
- Safety protocols (Class 4 laser hazards)
- Machine operation (software, movement controls)
- Material handling & nesting
- Parameter optimization (power, speed, frequency)
- Hands-on cutting practice
- Troubleshooting basics
Training Cost: AED 3,000-6,000 per operator
Plasma Operator Training (30-60 hours)
Initial Certification (30 hours):
- Electrical safety & high-voltage awareness
- Plasma arc physics
- Machine operation (controls, movements)
- Gas & consumables management
- Material handling
- Deburring techniques
- Hands-on practice
Training Cost: AED 2,000-4,000 per operator
Conclusion: Which Technology Should You Choose?
There is no universal winner. The right technology depends on your specific work:
Choose Laser If: You cut sheet metal <12mm with variety (aluminum, stainless, mild steel). You need precision, fast turnaround, and zero secondary finishing. Laser wins on speed, cost-per-part, and edge quality.
Choose Plasma If: You cut thick structural steel 30mm+. You need lowest upfront capital. Speed and precision aren't critical. Plasma excels on thick materials and budget.
Choose Both If: You run a modern, competitive job shop. Laser handles thin sheet variety work. Plasma handles thick structural work. Combined, they handle every metal fabrication challenge-making your shop capable of quoting jobs others can't.
Ready to Make the Right Choice for Your Shop?
Get a customized technology recommendation based on your actual production profile.